Product Description
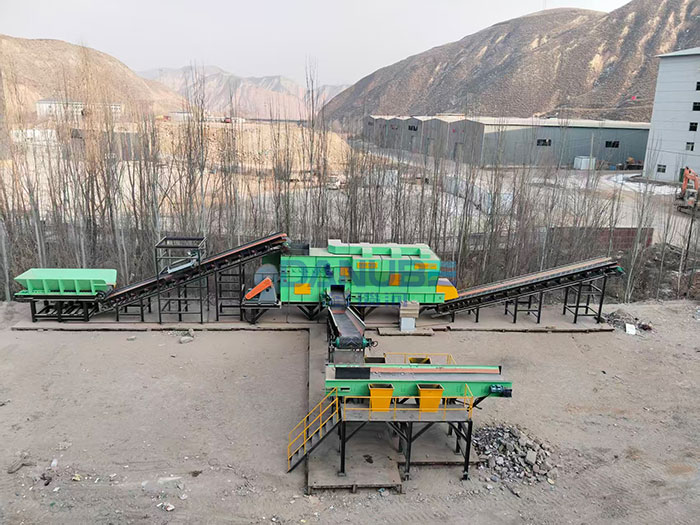
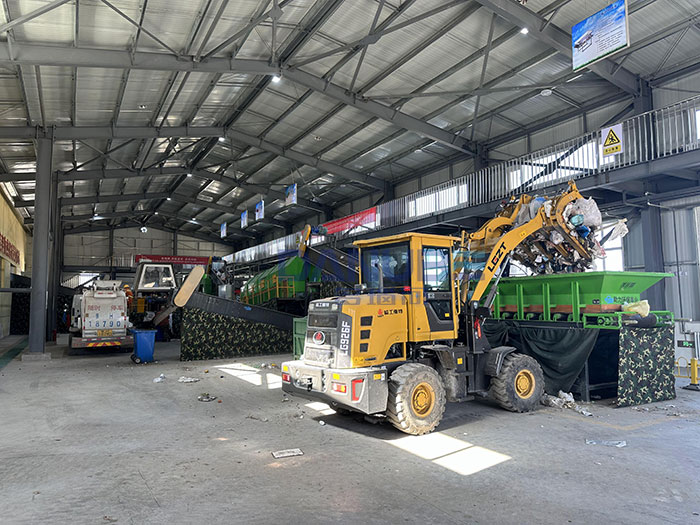
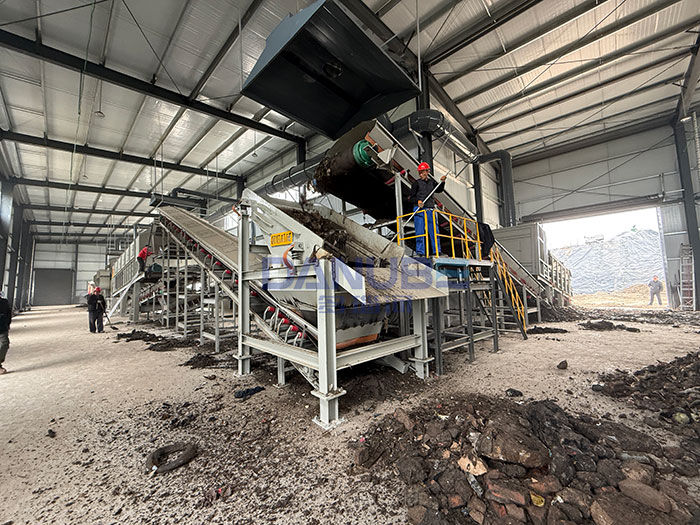
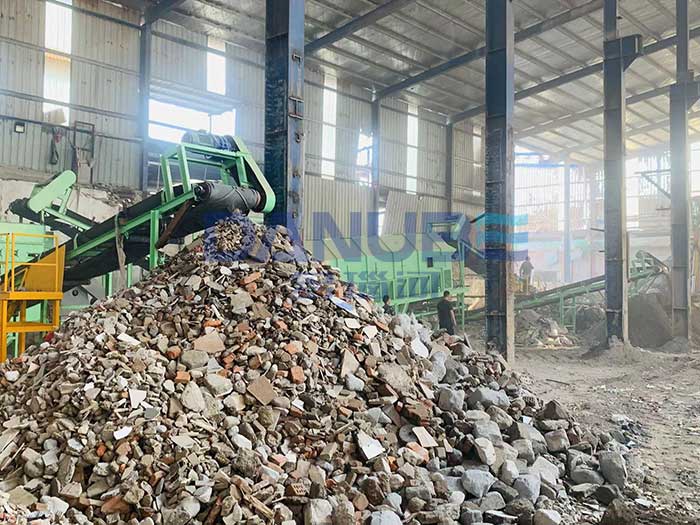
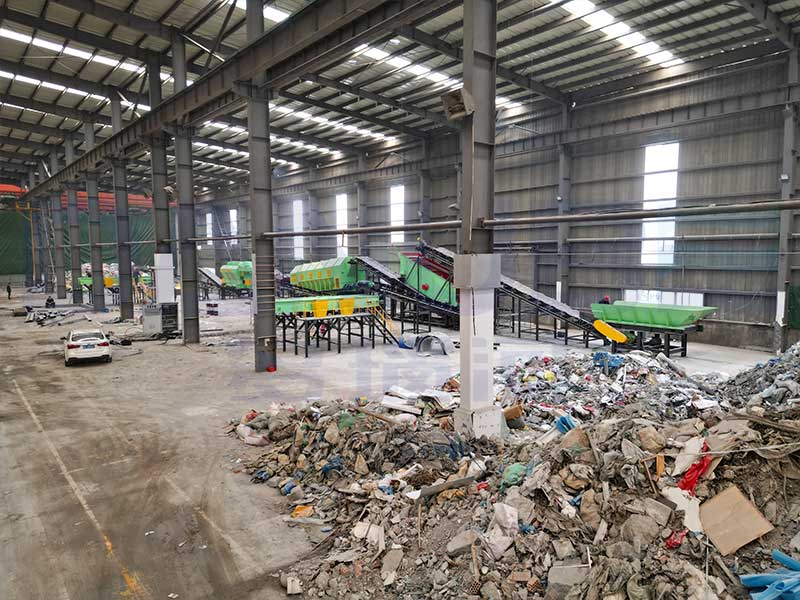
Material recovery facility (also called an MRF plant) consists of feeding, bag breaking, screening, sorting, shredding, and forming systems. Through bag breaking, screening, and sorting processes, metals, plastics, paper, textiles, and recycled aggregates can be separated, achieving resource recycling and effectively solving the pollution problems caused by municipal solid waste.
Features
1. High degree of automation, intelligent sorting, saving labor costs.
2. Complete process configuration, high sorting accuracy.
4. Strong processing capacity, stable operation.
5. Turning waste into treasure, reducing landfill and environmental pollution.

Process Flow
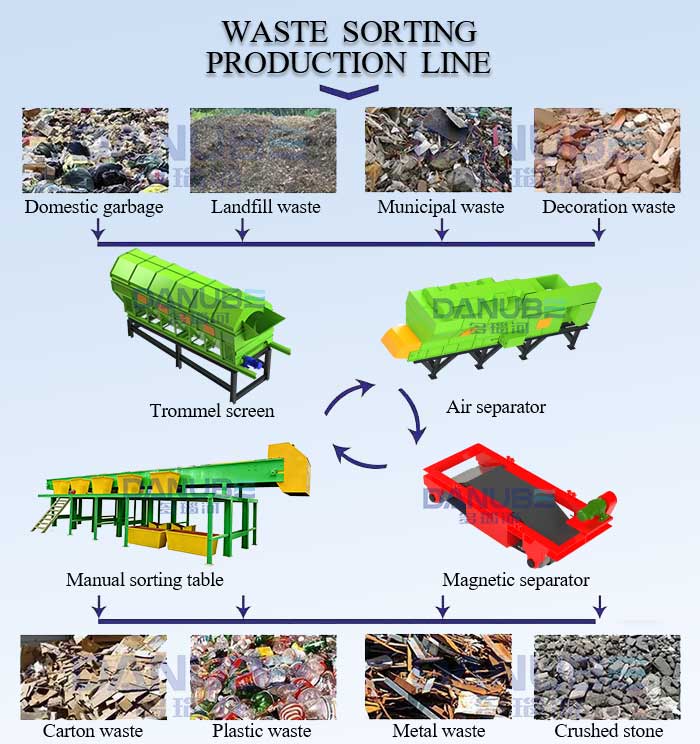
After entering the hopper, mixed municipal solid waste is conveyed by a chain feeder to a bag-breaking machine to remove packaging bags. It then enters a 30/50mm aperture drum screen to separate fine materials (<30/50mm) from coarse materials (>30/50mm).
Fine materials go through magnetic separation to remove metallic impurities, and the rest are stored for subsequent recycled aggregate processing. Coarse materials first enter an air separator to separate light and heavy materials, which then go to a manual sorting station to remove large debris and non-recyclable hazardous materials, separating into light materials (plastics, textiles, paper) and heavy materials (bricks, ceramics, etc.).
Unusable light materials for RDF fuel rods are baled; usable ones undergo magnetic separation, shredding, and RDF forming. Heavy materials are inspected, crushed and screened into reusable recycled aggregates.
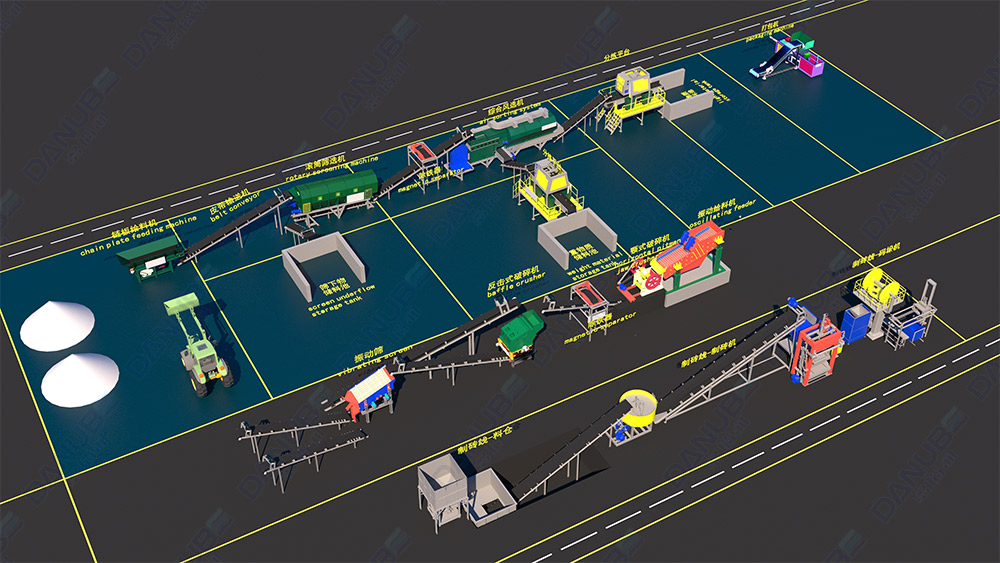
Component of Material Recovery Facility (MRF)

tel:0086 17596531123
email:danube@lantianmachine.com
address:No. 9 Yulian Industrial Cluster, Gongyi, Zhengzhou, Henan Province China
If you are interested in our products, Please enter the keyword you want to search
 EN | CN